Craftsmanship
How a Ugartechea is made
From the first, Ugartechea was a self-sufficient workshop: it bored its own barrels, did its own hardening, bluing and chroming, and stocked every gun in oil-finished walnut. This is how a gun comes together, from forging to proof.
01
Barrels
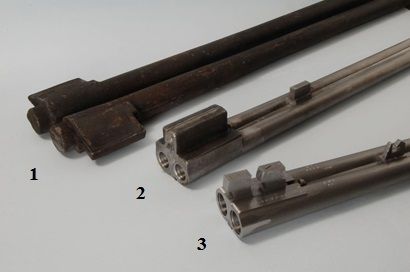
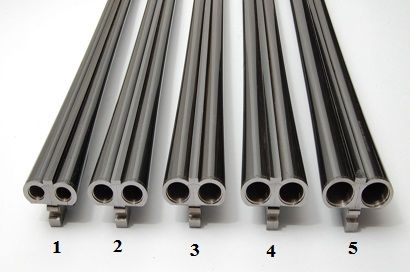
Each barrel begins as a steel forging. It is rough-turned, bored, machined and then joined to its partner and finished by hand. Ugartechea sidelocks use demi-bloc construction, in which each tube is forged with half of the lump that locks the gun shut.
Barrels are made in five gauges, from 12 to .410, and in lengths from 25″ to 28″.
02
The action
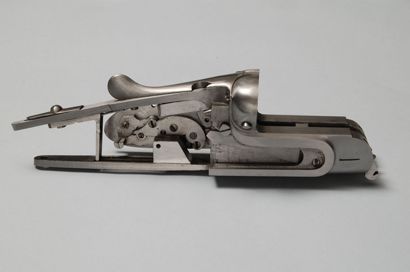
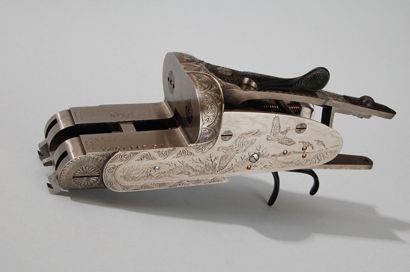
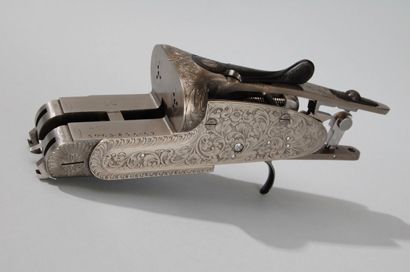
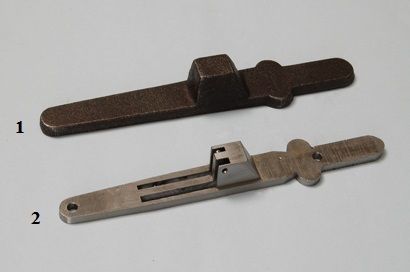
The action body starts as a forging too, and is machined in stages to its final form. Its interior is cut to take the lockwork, and it is fitted for double triggers or, to order, a single trigger.
03
Lockwork
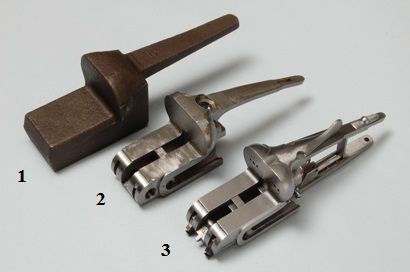
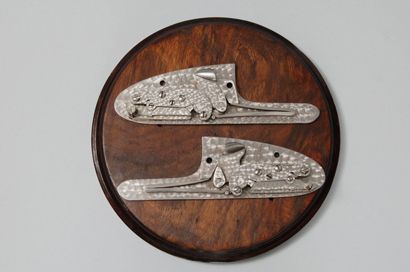
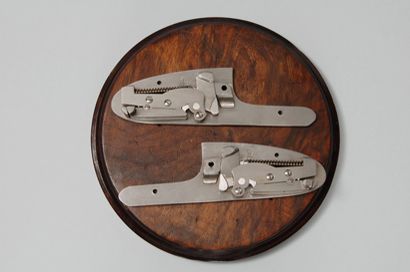
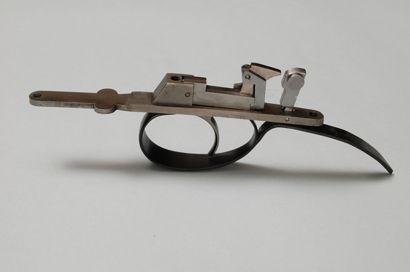
Locks are built with traditional V-mainsprings or with coil springs, depending on the model, and the sears are finished and regulated by hand for a clean, consistent pull. The trigger plate is machined from a rough forging and fitted to the action.
04
Stocking and finishing
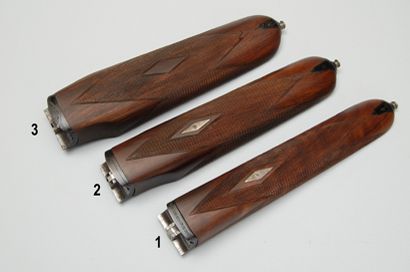
The walnut is selected for each gun, shaped to the customer’s dimensions, oil-finished and checkered by hand. Forends are made in English, semi-beavertail or beavertail form, and the rib (flat, concave or trapezoidal) is laid between the barrels.
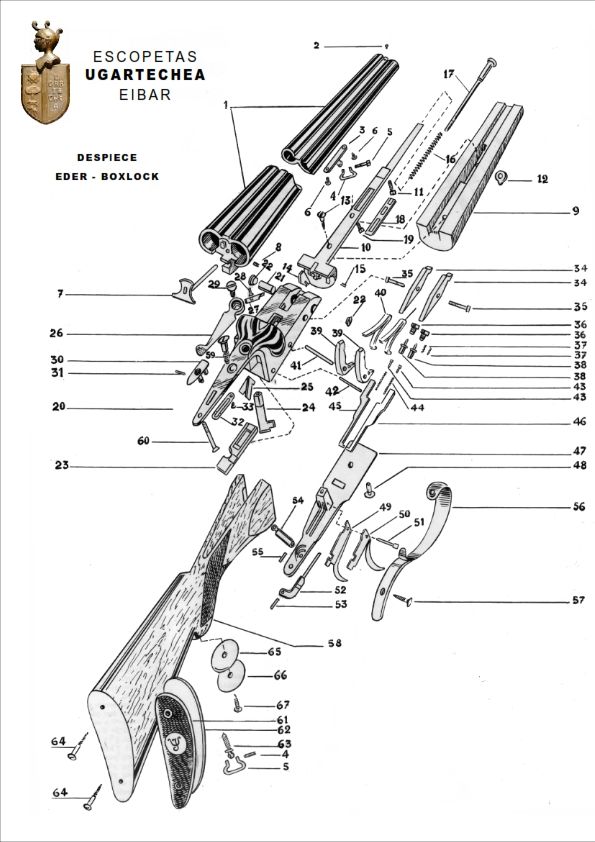
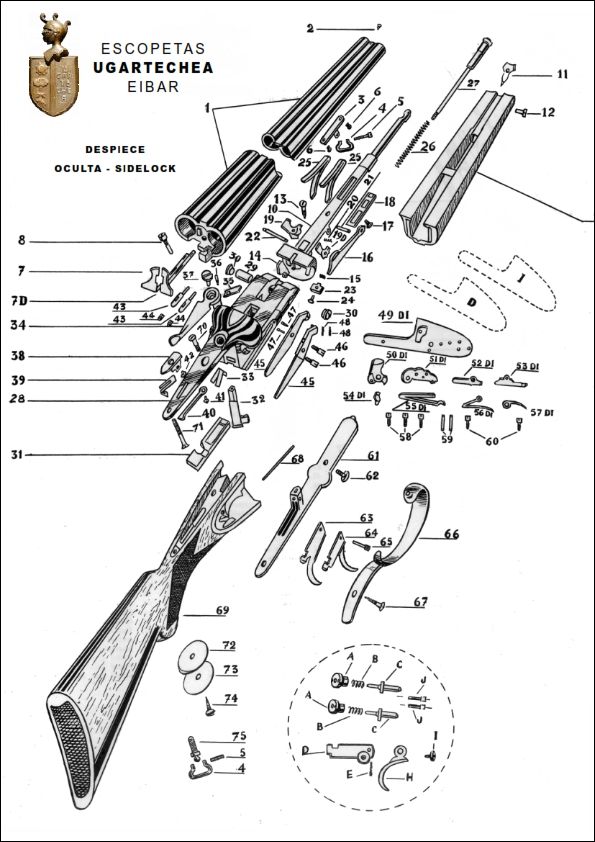
Every part, drawn
The factory’s exploded drawings of the boxlock (Eder) and sidelock (Oculta) actions. Owners can use them to identify parts for service.
Proof
Before it leaves Eibar, every gun is proofed at the Banco Oficial de Pruebas, Spain’s official proof house, and stamped with its proof marks under C.I.P. rules.
Contact
Talk to the workshop
Questions about a model, a specification or an order? Email us and the team in Eibar will reply, usually within one business day.